Level Switches
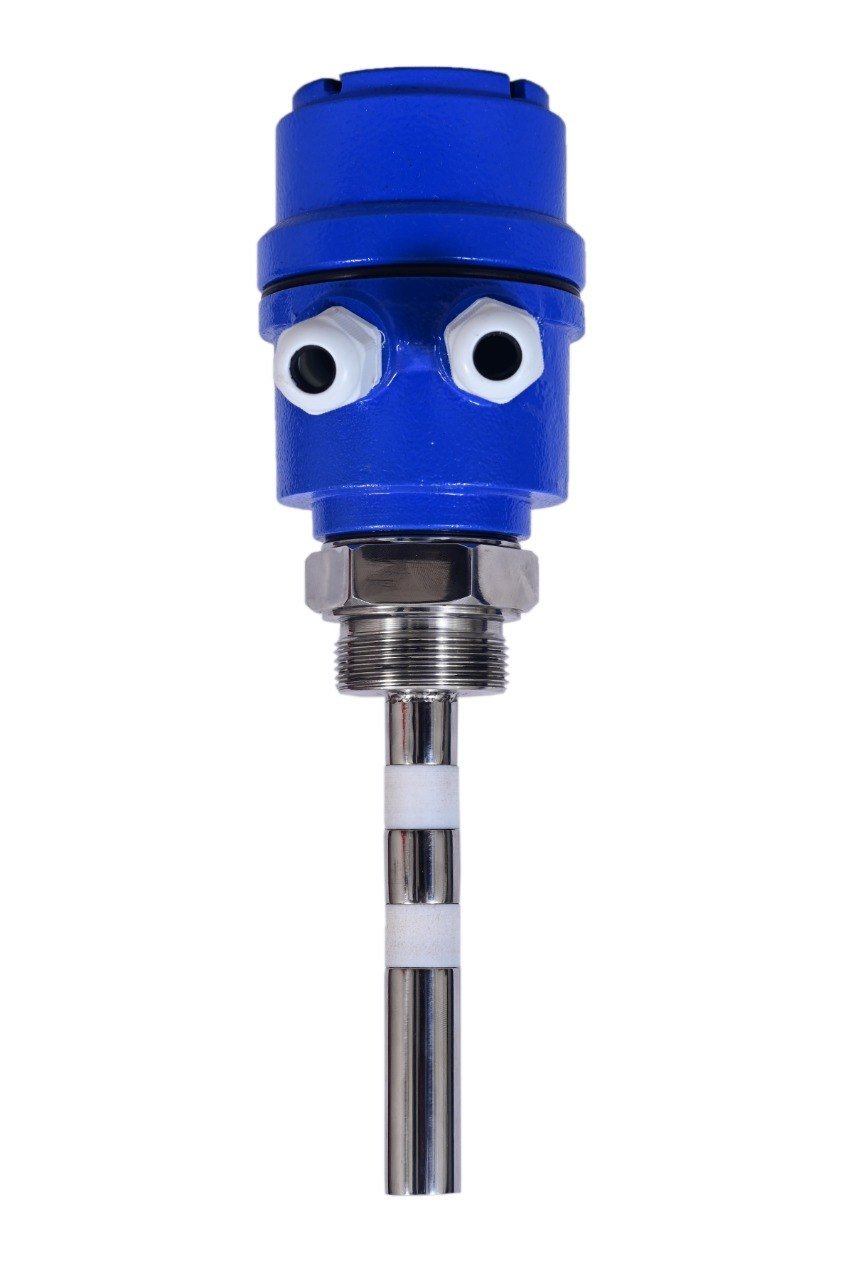
Anyone who has run a plant knows how much damage one overflowing tank or one empty hopper can do. A silo runs dry, a pump runs without liquid, and production stops. A reliable level switch is a small device that prevents these problems.
At Levtron Instrument Pvt. Ltd., we design and manufacture level switches for the people who keep Indian industry running. We are based in Pune, and we supply to factories, process plants and storage facilities across the country. Our range covers RF admittance, vibrating fork and heavy duty designs. It handles solids, powders, liquids and slurries, from a simple water tank to a deep cement silo.
What Is a Level Switch?
A level switch detects whether a material has reached a set point inside a tank, silo, hopper or pipe. When the material touches or approaches the sensing probe, the switch changes its output state. That signal can start a pump, close a valve, sound an alarm or stop a conveyor.
Unlike a continuous level transmitter, which reports the exact level at all times, a level switch answers one question: is the material at this point or not? That makes it simpler, cheaper and very dependable for high-level alarms, low-level cut-offs and process interlocks.
Why Choose Level Switch?
Plenty of plants still rely on manual dip-sticks, sight glasses or operator judgement. These methods work until someone is late, distracted or off shift. An automatic level switch does not have those lapses.
- It watches the material around the clock, with no one needed at the tank.
- It protects pumps, motors and mixers from dry running.
- It helps prevent spillage, product loss and cleanup costs.
- It costs far less than a full continuous measurement system when you only need point detection.
Choosing the right technology matters just as much. Our RF admittance switches ignore coating build-up on the probe. Our vibrating fork switch works well with free-flowing solids and many liquids. We help you pick the type that suits your material instead of selling you whatever is on the shelf.
Applications of Level Switch
Our level switches are used wherever material needs to be monitored and controlled:
- Cement and building materials: silos, hoppers and bins holding cement, fly ash and sand
- Food and beverage: flour, sugar, grain, milk and liquid ingredient tanks
- Chemicals and pharma: storage and process vessels for powders, solvents and slurries
- Water and wastewater: sumps, overhead tanks and treatment plant basins
- Plastics and polymers: granule and powder hoppers on moulding and extrusion lines
- Power and steel: coal bunkers, ash handling and chute monitoring
- Packaging and material handling: feed hoppers, chutes and conveyor transfer points
Salient Features of Our Level Switch
Our range has been built around real plant conditions, such as dust, vibration, sticky materials and tight installation spaces.
- Multiple models for different jobs: RFLS-100S and RFLS-100L compact versions for solids and liquids, the VFLS-200S vibrating fork, and the RFLS-300 series for tougher duties
- Special probe designs: full PTFE probes for aggressive liquids, rope type probes for deep silos, disc probes for chutes, and heavy duty probes for harsh environments
- RF admittance technology: stable detection even when material coats the probe
- No moving parts in the sensing area on most models: which means less wear and less maintenance
- Robust construction: built to cope with dust, temperature changes and continuous operation
- Easy installation: simple mounting and straightforward wiring
- Adjustable sensitivity: one switch can be set for different materials without replacing the unit
Benefits of Using a Level Switch
- Fewer breakdowns. Pumps and motors are shielded from dry running, and tanks are shielded from overfilling.
- Lower running cost. Automated control cuts the labour needed for manual checks and reduces product wastage.
- Safer operations. In chemical and dusty environments, fewer people need to climb tanks or open hatches to check the level.
- Consistent production. Hoppers stay filled and lines keep running, so you avoid unplanned stoppages.
- Long service life. A well-built switch with no mechanical parts in the sensing area can run for years with very little attention.
- Easy integration. The output works with PLCs, relays, alarms and control panels, so it fits into the setup you already have.
Level Switch Supplier In Pune
Levtron Instrument Pvt. Ltd. is a trusted level switch supplier in Pune. We are not a trader reselling someone else’s product. We manufacture our own switches, so we can answer technical questions directly and supply them promptly. We can also adapt a model when a standard one does not fit your application.
Our team looks at your material, tank size, process temperature and mounting position before recommending a model. We support customers in Pune, Pimpri-Chinchwad, Mumbai, Nashik and across Maharashtra, and we ship across India for projects of any size. Whether you need a single replacement unit or a batch for a new plant, we are happy to help.